Visitor
East curb cut off Old Gentilly. Loop at the demonstration pad. Park, walk The 1,250 first-article house. Factory tour is the showroom. A fence and a personnel gate are the only way onto the production yard.
Ameridura Manufacturing Company
Phase 1 platformRaw materials → finished home → delivery → erection → commissioning. The Gulf South’s ICF housing manufacturer — then every state whose modular program we certify into.
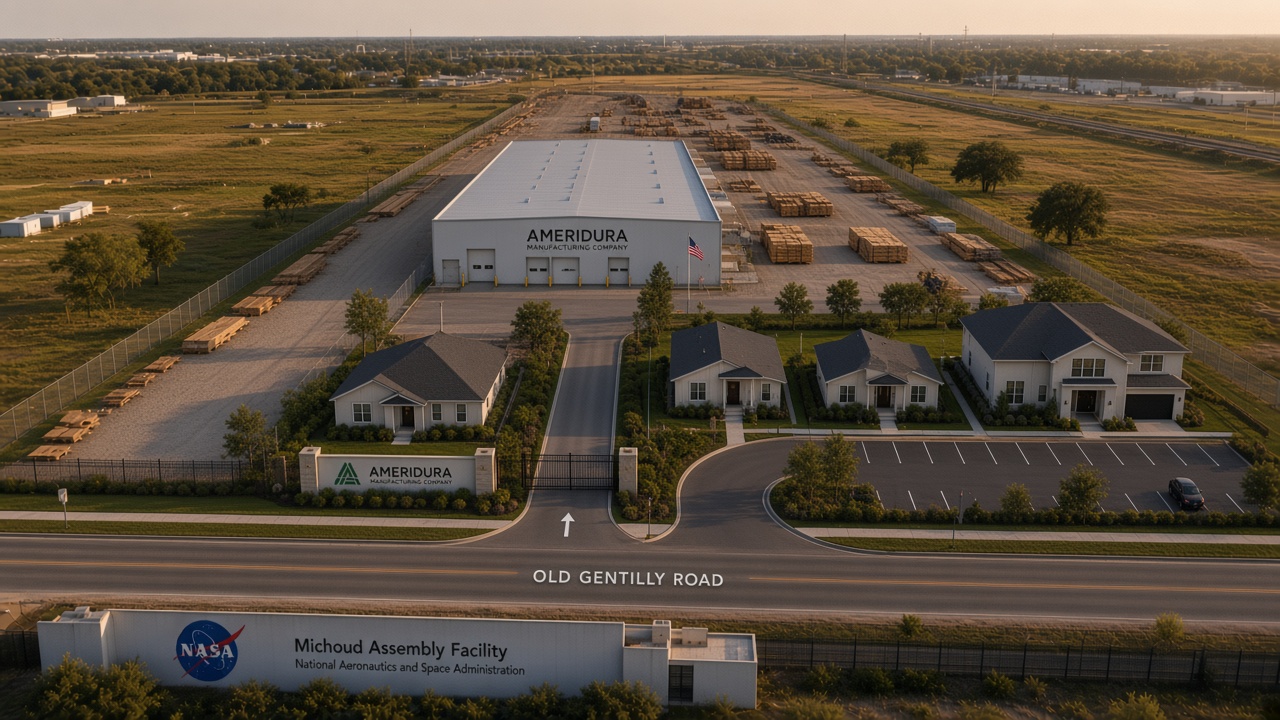
55197 fronts Old Gentilly about 207 feet and runs about 2,800 feet to the railroad. Phase I occupies the front 7 acres of that strip — about 1,472 feet of depth. NASA is across the paved street, not on this dirt. The remaining ~5.7 acres stay on the same parcel as yard / a later pad. $200,000 of site work is gravel, fence, lights, and short taps — not a palm-lined industrial park.
The demonstration pad is the public face: The 1,250 first-article house at the gate, a small lawn, visitor parking. Behind the fence the plant is ugly on purpose — high-bay, slab, crane, docks, gravel.
Visitor
East curb cut off Old Gentilly. Loop at the demonstration pad. Park, walk The 1,250 first-article house. Factory tour is the showroom. A fence and a personnel gate are the only way onto the production yard.
Truck
West curb cut. 28' gravel drive the length of Phase I. Receiving on the west wall. Four shipping docks on the north wall into finished-home staging. Turnaround at the north end of the trailer yard. Same drive back to Old Gentilly.
| From Old Gentilly, going north | Depth | Finish | Holds |
|---|---|---|---|
| Two driveways | 40′ | Curb cuts + gravel aprons | Visitor east. Truck west. Split at the property line, not inside a shared courtyard. |
| Model village + visitor parking | 220′ | The only lawn. Gravel visitor lot. | The 1,250 (The Beginning), The 1,500 (Room to Grow), The 1,850 Family Home as the sales office. ~20 visitor stalls. Not production mix. |
| Employee parking / office apron | 80′ | Gravel | Day-shift cars. Pedestrian door into the south office wall. No truck turning here. |
| 40,000 SF high-bay | 235′ | Industrial slab · 36' clear · gantry | Offices on the south wall. Two ICF cells, cassette tables, two assembly lanes, MEP supermarket. Two receiving docks west. Four shipping docks north. |
| Material yard | 180′ | Gravel + racks | ICF forms, steel, rebar, lumber, cassette kits. Forklifts only. Overhead lift stays inside the hall. |
| Finished-home staging | 250′ | Gravel pads | Completed modules on fixtures, short of the docks. Not a residential street of toy houses. Transport envelope is an engineering decision from each SKU. |
| Trailer / truck yard | 180′ | Gravel + hammerhead | Company trailers, inbound steel, overnight WIP. Turnaround so trucks do not reverse down 1,400 feet of drive. |
| Stormwater / buffer | 80′ | Ditch / basin as civil requires | Yard drainage. Not a lake amenity. Not a park. |
| Phase I expansion pad | 207′ | Cleared / rough grade only | Same-parcel future cell or second hall. Not lots. Not a street grid. Not this $5 million. |
The 55197 listing is ~207' of Old Gentilly frontage. A 200' × 200' square does not leave a truck drive. The 40,000-SF high-bay is ~170' × 235' — width set by the parcel, depth set by two assembly lanes and four north docks. A 300' × 100' bar is still the wrong geometry for this product. Phase I factory is engineered for scalable production with a target of up to 50 production-equivalent units per month following process validation, labor-hour reduction, station balancing and demonstrated throughput. Do not put “50/month guaranteed” in the lender plan. The credit-case P&L is still the operating ramp: 30 / 120 / 240 / 480 complete homes. 50 PE/month is the manufacturing design target after the line is proven.
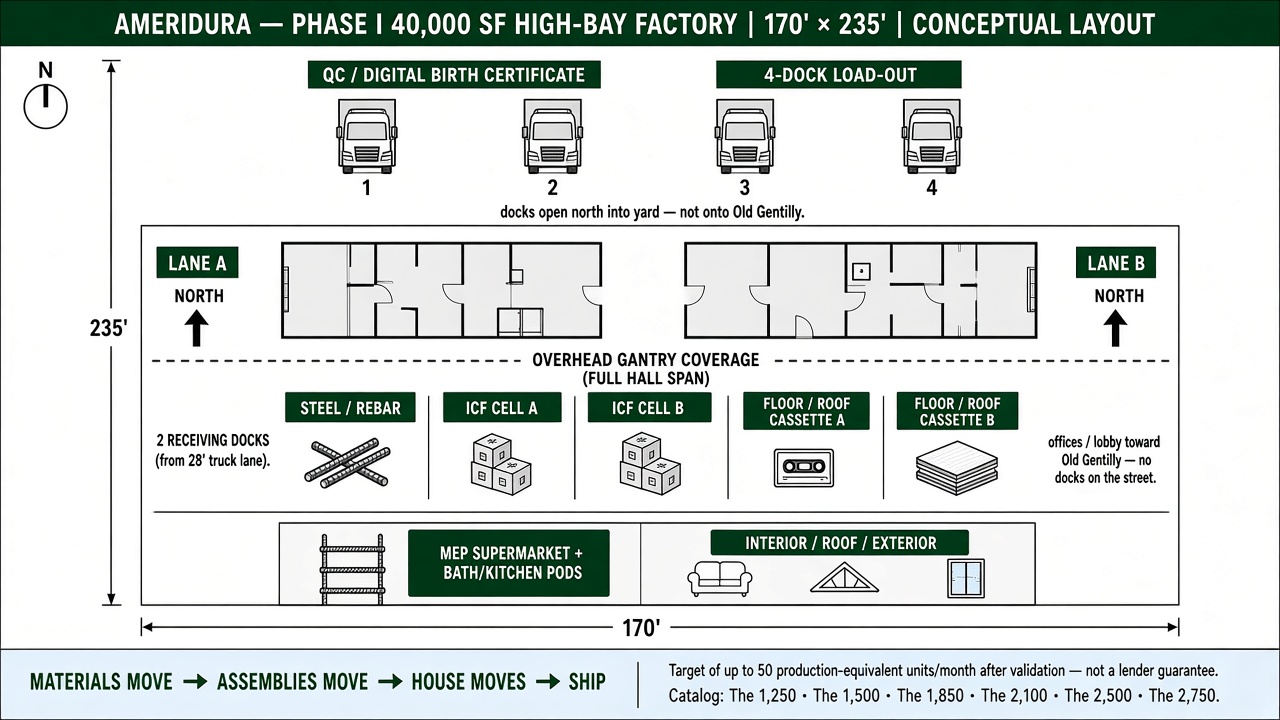
Do not park four complete houses side-by-side as the layout. That is what made the old renderings look fake. Two full-scale assembly lanes plus upstream cells is parallel production.
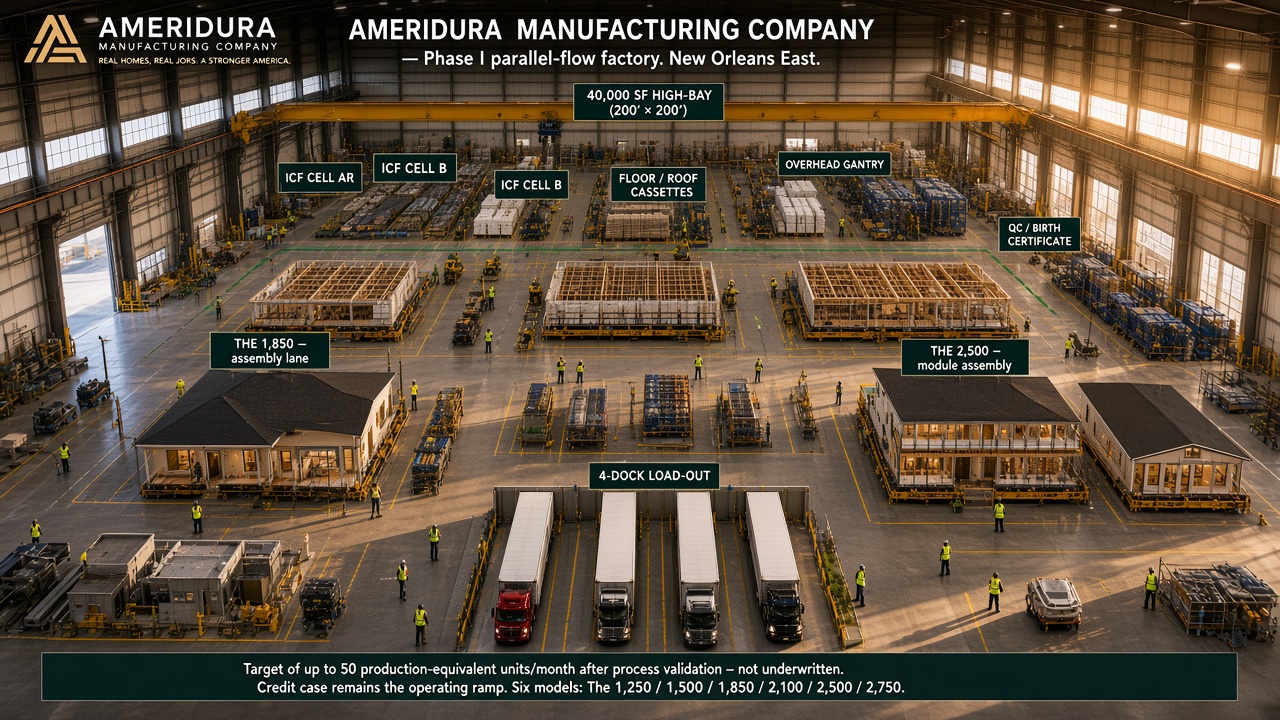
Everything does not move everywhere. Employees do not carry walls. A finished 2,500-SF house does not drive through the building.
Early — materials move
Steel, ICF forms, rebar, lumber, MEP kits. Forklifts, pallet jacks, carts. Overhead lift for heavy pieces.
Middle — assemblies move
Wall cassettes, floor cassettes, roof cassettes, MEP racks, bath/kitchen pods. Gantry / crane places them on the house. Workers stay in their zone.
House — fixture advances
The module sits on a heavy-duty production fixture / dolly. Station to station. The transfer mechanism is an engineering decision from actual SKU dimensions — not locked as an auto-plant conveyor.
Final — short move to QC and docks
Completed module moves a short distance to QC / digital birth certificate, then to one of four docks. Transport envelope is designed from the SKU, not from a 38-foot house on a normal trailer.
One house must not occupy the entire production system. While House A is structural, House B can take MEP, House C interiors, House D final assembly, House E QC — and the next houses’ ICF, cassettes, and pods are already being made.
Two ICF cells
If ICF is a single bottleneck, the factory stops. Cell A and Cell B run together.
Parallel floor / roof cassettes
Built off the house line. Ready when the module reaches assembly.
MEP supermarket
Harnesses, manifolds, ducts, racks — built ahead, delivered to the station.
Bath / kitchen pods
Repeatable assemblies. The bathroom is an assembly, not a jobsite.
Two full-scale assembly lanes
Workers come to the house. Overhead gantry covers the hall.
QC / birth certificate / four docks
AI inspects 100%. Humans handle exceptions. Load-out is a designed ship system.
Intelligent Manufacturing Lab (1,360 SF)
Inside the hall. PLC, vision, BIM, digital twin. Not a separate STEM building. Job: remove labor-hours from the house.
Do not spend the shell budget making the warehouse prettier. Ugly and perfectly functional beats a beautiful building with inadequate production infrastructure.
| Zone | Depth | SF | Holds |
|---|---|---|---|
| Steel · ICF A/B · floor/roof A/B | 50′ | 8,500 | Two ICF cells so pour/cure is not a single bottleneck. Cassette tables off the house line. |
| Full-scale assembly lanes A & B | 110′ | 18,700 | True-scale modules on fixtures, running the 235' depth. Gantry coverage. Worker clearance, aisles, fire lanes. |
| MEP / pods · interior · roof / exterior | 32′ | 5,440 | Supermarket, bath/kitchen pods, roof and exterior packages. Built ahead of the house. |
| Intelligent Manufacturing Lab | 8′ | 1,360 | 1,360 SF inside the hall: PLC, vision, BIM, digital twin, small arm. Not a separate STEM building. |
| QC / digital birth certificate · 4-dock load-out | 35′ | 5,950 | Inspection is a gate. Four north docks open into finished-home staging — not onto Old Gentilly. |
More homes per employee, fewer touches per home, fewer mistakes, less WIP, less material waste, and higher first-pass yield.
Ameridura has engineered the ICF house as a digitally native product that can be configured, engineered, fabricated, inspected, documented and shipped through an increasingly automated manufacturing system. The house is the product. The factory is the machine that repeatedly produces it.
Staffing scales with production and is controlled through standardized processes and automation. Year-one roster remains 46 commissioning seats. Do not tell the lender AI eliminates half the workforce. Produce the same output with progressively fewer labor-hours. 400 is the starting line. 350 → 300 → 275 → 250 are engineering targets, not claims.
Level 1
AI
Thinks, optimizes, predicts, and generates jobs. Does not drive a robot.
Level 2
MES / factory software
Turns those jobs into released production work.
Level 3
PLC / industrial controller
Executes a validated program on the machine.
Level 4
Machine / robot
Cuts, places, moves, or fastens.
Level 5
Sensors + computer vision
Verify that it happened inside tolerance.
Level 6
Human
Exceptions, safety, PE stamp, quality disposition, final accountability.
Every month, manufacturing engineering asks what ten labor-hours can be removed from the standard house. 10 hours × 600 homes/year = 6,000 hours. Repeat. That is the culture — not a robot announcement.
| Stage | Hours / home | Status | Honesty |
|---|---|---|---|
| First article | 920 | measured | The 1,250 laboratory house. Replace assumptions with minutes. |
| Mature baseline | 400 | underwritten | Lender operating standard at one and two shifts. |
| Optimization | 350 | target | Year-2 engineering target after first-pass yield exists. |
| Advanced automation | 300 | target | The problem to attack — not a promise on this note. |
| Long-term | 225 | investigation | 200–250 band. Not in the credit-case P&L. |
Not humanoids. Not a $500k AI-factory brand. Automation that attacks labor-hours per house.
| Cell | Budget |
|---|---|
| Automated material movement (AMR / carts / dollies / tracking) | $115,000 |
| Computer vision / QC (AI inspects 100%; humans handle exceptions) | $90,000 |
| Automated kitting | $70,000 |
| AI-guided work stations | $45,000 |
| Assisted ICF cell (position, clamp, adhesive, dimension — not a house robot) | $90,000 |
| Assisted steel / rebar processes | $70,000 |
| Sensors / predictive maintenance | $35,000 |
| Controls / PLC integration / commissioning | $35,000 |
| Phase I automation envelope | $550,000 |
Day-1 intelligent factory is approximately $1.2 million of overlapping spend already inside the $5 million uses — core CNC, $550k automation cells, $200k digital backbone, sensors, and integration. It is not a second $1.2 million on top of the ceiling. The ~$3.6 million mature vision is Phase II/III after the line produces data.
Full vision $2.9M–$4.5M (planning midpoint $3,600,000). Complete software-defined factory. Not spent on this note. Not 100 robots. Not a humanoid. Phase II/III after labor-hours/home, scrap, defects, cycle time, downtime, and station bottlenecks are measured.
I — AI-native foundation
$1.0M–$1.4M
Factory opens digitized. Humans still run most cells.
II — serious automation
$0.9M–$1.4M
Largest labor constraints removed.
III — near-autonomous cells
$1.0M–$1.7M
Highly automated factory. Still not a promise of 50 homes/month.
Automate the worst jobs first
1,000–1,500 SF inside the 40,000-SF high-bay (1,360 SF on this layout). Not a separate $1M STEM building. Not an extracurricular robot classroom. Remove labor-hours from the house. Students and vendors can work here later. The factory gets the savings first.
Reduce ICF assembly labor 30%
Automate material movement
Computer vision QC
AI production scheduling
AI MEP kitting
Digital twin of the factory
Predictive maintenance
AI engineering assistant
AI purchasing
Autonomous warehouse
Phase I manufactures The 1,250, The 1,500, The 1,850, The 2,100. The 2,500 and The 2,750 stay fully engineered — BIM, BOM, routing, price — and turn on when the market asks. The customer sees four houses. The factory sees one construction system.
The 1,250
First article / USDA entry / cost laboratory
The 1,500
Hero / Phase I volume model
The 1,850
Family workhorse — four bedrooms
The 2,100
Move-up / premium family
The 2,500
Engineered on-deck — turn on when demand asks
The 2,750
Engineered on-deck — turn on when demand asks
| # | Opportunity | Phase I | Later |
|---|---|---|---|
| 1 | AI production scheduler | MES + dashboard on Day 1 | Closed-loop station resequence when a cell falls behind |
| 2 | Computer vision QC | Cameras at critical stations; AI flags; humans disposition | 100% automated inspection coverage |
| 3 | Digital birth certificate | House serial, lots, photos, QC, MEP tests | Appliance serials, torque, scans, field history |
| 4 | Robotic material movement | Smart carts, dollies, gantry, tracking | AMR / AGV fleet when utilization pays |
| 5 | BIM → CNC with zero interpretation | Cut lists from the model | CAM released without a human redraw |
| 6 | AI nesting | Nesting on foam, sheet, steel | Multi-house scrap minimization |
| 7 | Automated rebar / steel cell | CNC bend/cut + labeled kits | Coil-to-kit cell |
| 8 | ICF micro-automation | Jigs, clamp, adhesive, dimension assist | Operator-supervised cell, not a house-building robot |
| 9 | Vision-guided robots | Not Day 1 | 2–3 cells after the job is proven repetitive |
| 10 | Automated MEP prefab | Harness / manifold / duct stations | Wet-core modules build-test-scan-install |
| 11 | Kitting system | House kit from the BOM | Warehouse assembles without walking |
| 12 | RFID / vision inventory | Barcode + house serial | Lot → kit → station → house |
| 13 | Predictive maintenance | Sensors on CNC, crane, air, critical tools | Failure predicted into scheduled downtime |
| 14 | AI energy management | Metered later | Load-shift compressors and cells |
| 15 | AI worker guidance | Station tablets, scan-complete | Torque and vision close the step |
| 16 | AR work instructions | Tablets | Glasses where they earn |
| 17 | AI engineering assistant | On Autodesk seats; PE stamps | Clash, BOM, revision grunt work |
| 18 | AI purchasing agent | BOM vs inventory vs lead time | Routine POs inside limits |
| 19 | AI sales / configuration | Model → size → ZIP → options → price | Feasibility + BIM from the sentence |
| 20 | Factory brain | One dashboard: orders, stations, defects | What is stopping the next house? |
Design the house from the manufacturing line backward. Simple rectangular footprints, fewer corners, standardized openings, and planned penetrations reduce ICF labor, bracing, waste, and complexity. Finish packages create luxury. Structural geometry does not.
All 50 states is a certification, plan-review, inspection, licensing, and installation program — not a machine purchase. Modular programs commonly require manufacturing-facility licensing, a quality-assurance manual, model/state plan approval, and ongoing inspections.
You buy foam shapes, steel joists, and — if soils need them — helical piers. That is how every housing plant works. You do not wait to own those factories to ship a house.
Phase I builds every catalog SKU: The 1,250, The 1,500, The 1,850, The 2,100, The 2,500, and The 2,750. There is no 640-SF house. A finished Ameridura Home leaves the 40,000-square-foot plant — ICF walls assembled, poured and cured; floor cassette built on our tables; roof cassette; wet core; electrical; HVAC installed; cabinets; baths; openings; finishes; QC serial; load-out; truck to the pad. That is the manufacturer. Toyota does not own the steel mill. Ford does not own the tire plant. Ameridura does not own Benchmark’s foam press, Bailey’s joist mill, or PierTech’s pier plant — and still manufactures the house.
The $5,000,000 already buys the house line: CNC / hot-wire, wall jigs, CNC rebar bender, plasma table, floor and roof tables, wet-core cell, cabinet CNC, handling, and fleet. A foam press, a joist mill, and a pier factory would displace that line if they were crammed into the same note.
| Catalog SKU | SF | What leaves the plant |
|---|---|---|
| The 1,250 — The Beginning | 1,250 | Complete house. First article and street-front walk-through. |
| The 1,500 — Room to Grow | 1,500 | Complete house. Day-1 walk-through. |
| The 1,850 — The Family Home | 1,850 | Complete house. Volume house and sales office. |
| The 2,100 — More Room for Life | 2,100 | Complete house. Rotates onto the showcase later. |
| The 2,500 — Signature | 2,500 | Complete house. Two-story. Same stations. One of six. |
| The 2,750 — The Legacy | 2,750 | Complete house. Two-story. Rotates onto the showcase later. |
You manufacture the house. Foam, joists, and piers are bought-in parts with engineered specs — not a confession that the plant cannot build. Walls, floor, and foundation interface are taken from listed assemblies, not from a private code and not from a jobsite invention. Foam shapes come from a molder working to PE drawings. Floor joists are roll-formed cold-formed steel, specified to work with ICF. Where soils need it, the house sits on helical piers. Architects and engineers stamp to the ICC family as the destination state adopted it. Ameridura takes what that stack already lists. It does not write a substitute code.
The product is the line: The 1,250, The 1,500, The 1,850, The 2,100, The 2,500, and The 2,750. Every model is factory-built ICF modular, IRC as adopted by Louisiana, set on a permanent foundation. Developers, production builders, and contractors buying as builder of record pay $112 per living square foot at the factory gate. Louisiana families pay $125 per living square foot. Realtors are a lead source inside the family channel, not a separate housing channel.
Ameridura manufactures a six-model ICF housing line on one set of stations: The 1,250, The 1,500, The 1,850, The 2,100, The 2,500, and The 2,750. Phase I produces the first four. The 1,500 is the hero / volume model. The 1,250 is first article. The 2,500 and The 2,750 stay fully engineered on-deck — BIM, BOM, routing, price — and turn on when demand asks. There is no 640-SF house. Finish packages change appearance. The structural SKU does not. Production mix follows purchase orders.
| SKU | Model | SF | Stories | FY2027 | Role |
|---|---|---|---|---|---|
| AM-1250 | The Beginning | 1,250 | 1 | 8 | First-article production unit and cost laboratory. |
| AM-1500 | Room to Grow | 1,500 | 1 | 10 | Hero / Phase I volume model. Young family. Compact office. |
| AM-1850 | The Family Home | 1,850 | 1 | 8 | Family workhorse. Four bedrooms that actually work. |
| AM-2100 | More Room for Life | 2,100 | 1 | 4 | Move-up. Dedicated office. |
| AM-2500 | Signature | 2,500 | 2 | on order | Engineered on-deck. Two-story family. Same stations. Turn on when demand asks. |
| AM-2750 | The Legacy | 2,750 | 2 | on order | Engineered on-deck. Five-bedroom two-story. Activate when the 2,100 is not enough. |
| Rank | Formula | Cost | Appeal | Factory | Verdict |
|---|---|---|---|---|---|
| 3 | 2,500 SF single-story ICF + shingle | Very good | Excellent | Excellent | Very good production house, not the cheapest 2,500. Huge foundation, huge roof, large lot, more perimeter. First rendering energy — not the locked platform. |
| 1 | 2-story ICF + conventional shingle / factory cassettes | Excellent | Excellent | Excellent | Locked base. Cuts foundation and roof roughly in half versus the ranch. Factory makes the second floor and the roof as tables, not field puzzles. |
| 2 | 2-story ICF + factory roof cassette (named) | Excellent | Exceptional | Exceptional | Sweet spot of the roof debate. Included in Formula 2 as the standard roof method. |
| 1A | Hybrid ICF + factory cassettes | Potentially best | Exceptional | Exceptional | This is Formula 2 with the garage taken out of the concrete shell. Locked. The customer does not care that the garage is not ICF. They care that the house is. |
| 5 | 2-story ICF + concrete / ICF roof (FORTRESS) | Fair | Exceptional | Fair | Incredible product, not the cheapest. Shoring, pumping, extra structure, extra handling. Offer after base economics are proven. Do not make it Day-1 standard. |
Manufacture the complete house on this floor. Do not manufacture every commodity that goes into it. Foam shapes, mill steel, glass, HVAC equipment, appliances, and helical piers are purchased inputs — the same way a car plant buys steel and tires. Make the assemblies that give cost, speed, quality, and IP advantage.
Make (Phase 1)
Buy always
Never make
Do not buy a single major machine until the production system is designed.
Ameridura manufactures on the industrial 3D stack: Autodesk BIM, OpenUSD interchange, NVIDIA compute. Every house has a digital twin. The Alliance for OpenUSD is the standard. NVIDIA Inception is the program.
Ameridura’s digital plant is industrial production: configuration → Autodesk BIM → OpenUSD interchange → PE release → BOM → cut list → production → QC → shipping → digital twin of every house. Autodesk authors. NVIDIA computes. Alliance for OpenUSD is the standard — Pixar, Adobe, Apple, Autodesk, NVIDIA. NVIDIA Inception is the manufacturer program. Khronos glTF delivers the dealer configurator. OpenTofu pins plant infrastructure. Nix pins the toolchain. The PE stamps. A frozen plate stays frozen. The house is the product.
Alliance for OpenUSD founding members: Pixar · Adobe · Apple · Autodesk · NVIDIA
Ameridura is an NVIDIA Inception manufacturer. The digital plant — configurator, BIM, OpenUSD twin, production data — runs on the NVIDIA industrial stack. Application is free, no equity, no cohort. CTO and CEO file after EIN and the live site. Credits and preferred hardware pricing are operating. They do not replace the booked Autodesk seats and they do not fund the $5 million uses.
Customer configurationAutodesk BIM / CADOpenUSD digital twinEngineering release — PE stampBill of materialsPurchasing / inventoryCNC / work instructionsProduction stationsQC / serial recordLoad planTransportSite erectionCommissioningCertificate of occupancy interfaceWarranty / digital home record
| Department | Phase 1 | Later |
|---|---|---|
| Engineering + digital factory A change to the house model must flow into materials, quantities, labor, machine time, cost, and schedule. | BIM/CAD workstations, ERP/MES/QMS/CRM starter stack, plotter, barcode, shop tablets, NAS, firewall. | Full MES with station-level genealogy, RFID, AI optimization, machine-data historians. |
| Raw-material receiving Nothing is manufactured until it is received, inspected, labeled, and stored. | Docks, forklifts, racks, incoming inspection, barcode. | Truck scale, AGVs, automated conveyors. |
| ICF / EPS production ICF is the structural product. Day 1 we assemble purchased forms. Day 2 we mold our own. | Assembly tables, hot-wire/CNC foam cutters, jigs, bucks, labeling. Buy proven ICF forms. | Full EPS plant: pre-expander, silos, steam, shape molding (SPZ-140TE class or U.S. equivalent), mould family, recycling, palletizing. Not Phase I. |
| Steam + utilities plant Required for EPS molding. Not bolted on later without site design. | Compressed air, electrical service, dust collection, welding exhaust, backup generator. No steam boiler. | Industrial steam boiler ~1,000–2,000 kg/hr class, condensate, cooling tower — sized to the selected molder. |
| Rebar fabrication Reinforced concrete houses. In-house kits are a cost and quality advantage. | Cutter, CNC bender, stirrup bender, tying, cages/jigs, tagging. | Coil automation, mesh welding, robotic tying. |
| Steel fabrication Connectors, embeds, stairs, rails, transport/erection hardware. | Plasma, ironworker, saws, press brake, MIG/TIG, fume extraction. No fiber laser, no powder line. | Fiber laser, tube laser, robotic weld, blast/paint/powder. |
| Floor + roof systems The wall system cannot be the only factory product if the plant is going to beat site-built cycle time. | Cassette tables, CNC panel saw, routers, pneumatic fastening. Floor joists specified as Bailey TotalJoist / Speedfloor-class CFS, purchased cut-to-length until a roll-former earns its keep. Roof stays engineered wood cassette as standard. | In-house CFS joist roll-forming when volume pays. Composite steel-deck / lightweight concrete floors (Speedfloor / TotalJoist composite class) as an engineered option, not the Day-1 Bayou lid. |
| Wall assembly line This is where the plant behaves like an automobile plant. | Stations: layout, ICF, rebar, electrical, plumbing, bucks, embeds, QC. Jigs, lasers, tablets. | Robotic fastening, vision QC, automated material delivery. |
| Concrete ICF walls are assembled in the plant; structural concrete is generally placed after erection. | Field placement tools, vibrators, screeds, test kit. Ready-mix purchased. Mobile mixer option. | In-house batch plant, silos, reclaim — only when volume pays for it. |
| Windows + doors Do not melt glass. Do assemble and weatherproof the opening package. | Assembly tables, suction lifters, sealant, hardware stations. Buy IGUs and certified components. | Full window line if volume and certification economics support it. |
| MEP prefab Racks and pods instead of trades wandering a house for days. | Wire cut/strip, harness boards, conduit, PEX manifolds, duct brake/Pittsburgh, test equipment. | Automated wire processing, full bathroom pods, refrigerant charging cell. |
| Kitchen + bathroom prefab A bathroom should leave as an assembly, not a construction project. | Scaled cabinet cell (panel saw, edgebander, assembly). Buy stone/quartz cut. Shower/waterproofing station. | CNC stone, waterjet, dedicated bathroom-pod line. |
| Finishing Factory finishes are how the house ships closer to occupancy. | Drywall tools, spray booth, flooring/tile station, exterior package tables. | Automated taping, robotic paint. |
| Material handling The plant dies without lift, rack, and dock capacity. | Forklifts, pallet jacks, gantry/jib, vacuum/panel lifters, racks, docks. | Bridge crane, AGVs, overhead transport. |
| Quality-control laboratory National manufacturer, not a local prefab shop. | Dimensional, concrete field tests, electrical, plumbing pressure, blower-door, IR, moisture, weld/rebar inspection. | In-house compression frame if volume warrants; tensile via accredited lab until then. |
| Test house / destructive program Own the engineering/testing program. Partner with accredited labs for the expensive machines. | Dedicated pad and first test/prototype house in the inventory budget. Lab partnerships. | Wind/water/impact/fire partner program expanded; R&D building. |
| Factory automation National-scale quality is genealogy: House #001234, every lot, every station. | Barcode, tablets, digital work instructions, starter MES. No robotics. | Robotic weld/handling/paint/palletize, machine vision, OCR. |
| Shipping + logistics Transportation is part of the manufacturing system. | 2 tractors, flatbeds/step-deck, securement, GPS/ELD, permitting. | Regional hubs: Southeast, Texas, Midwest, Northeast, Mountain West, West Coast. Do not ship every house from Louisiana forever. |
| Field installation The factory is not finished when the truck leaves. | Foundation crew equipment, telehandler, contracted crane with budgeted access, lifts, commissioning tools. | Owned crane if utilization pays; regional installation teams. |
| Maintenance Downtime costs more than spare parts. | Welder, mill/drill/press, diagnostics, spare motors/sensors/PLC/pneumatics. | Full machine shop, CMMS maturity, predictive maintenance. |
| Safety system OSHA machine guarding, point-of-operation protection, anchoring, LOTO. Not optional. LWC On-Site Consultation at commissioning; SHARP after ≥1 year of rates — not claimed. | Guarding, e-stops, LOTO, fall protection, eyewash, PPE, SDS, fire extinguishers, forklift charging area. EHS Coordinator hired with live equipment. Comprehensive LWC consultation visit when the line is stood up. OSHA 300 logs from hour one. | SHARP application after a year of DART/TRC below industry average; Pre-SHARP if LWC puts us in that lane. Light curtains on automated cells, expanded suppression tied to EPS plant. Do not skip the booked kit because recognition exists on a webpage. |
| Fire / environmental / industrial infrastructure The building does not run without utilities and EHS. | Sprinkler/alarm in the 40,000 SF shell, ventilation, dust, welding exhaust, drains, spill kits, stormwater in site budget. | EPS VOC/steam, oil/water separator upgrades, larger fire-water. |
| The building itself Equipment is useless if the building is not designed around production. | 40,000 SF on 7 acres. Offices, lab, maintenance, docks, high doors, industrial slab. | 60,000–100,000+ SF, 30'+ clear, second line, EPS building, training center. Do not spend that money on Day 1. |
| National certification department There is no machine that makes the house legal everywhere. | VP Quality & Regulatory + contracted PE stamps, Louisiana first, 50-state matrix started, QA manual, installation manuals. | In-house code specialists for every region; HUD pathway only if deliberately chosen. |
| Quality management system Every house gets a digital birth certificate. | Document control, NCR, CAPA, incoming/in-process/final inspection, calibration, traceability, warranty log. ISO 9001 later. | ISO 9001 certification, supplier quality engineers, field-failure analytics. |
| Supply chain National volume contracts are where cost advantage gets serious. | Purchasing lead, starter contracts, $300k initial inventory. | National agreements on EPS, cement, rebar, windows, HVAC, appliances. |
| Product library Do not let customers design completely custom houses. Manufacturing efficiency lives in a short SKU list. | Four factory models. First article remains The 1,250. Hero / volume house is The 1,500. | Duplex 2400 / 3000 and regional wind/snow/seismic packages. |
Phase 1 — $5M launch platform
Capital close through first-year production
Does
Does not
Phase 2 — vertical integration
After the plant is selling homes in volume (hundreds, not a handful)
Does
Does not
Phase 3 — national manufacturer
After the Louisiana platform is proven
Does
Does not
This loan is the house factory. Foam moulding, batch plant, apartment/hotel pods, and every robot that actually earns a cell are named on the full in-house stack — not stuffed into $5,000,000.